Why hot condensate is worth more than cold make-up water
When steam gives up its heat in a calorifier, heat exchanger or process line, it turns back into hot condensate. That water still carries useful heat, often at 70 to 90 degrees C, and it has already been treated for boiler use. Sending it down the drain means the boiler must heat cold municipal water or borehole water all over again.
In Gauteng, where water quality can change from one supply point to the next, that matters. Every cubic metre of recovered condensate reduces the amount of fresh water you buy, the treatment you dose and the energy you burn. On plants running through load-shedding and recovery periods, that extra efficiency helps keep steam available without pushing the boiler harder than needed.
What condensate recovery saves on a working plant
The direct saving is fuel. The boiler uses less gas, diesel or electricity when the feedwater enters hotter. The second saving is water, and in many sites that is the bigger line item when production runs long hours. There is also a saving on chemicals because less make-up water means less oxygen scavenger, pH control and softener capacity.
- Lower boiler fuel use because feedwater enters at a higher temperature
- Less municipal or borehole water consumption
- Reduced chemical dosing and blowdown stress
- Less thermal shock on feed tanks, pumps and boiler tube plates
- Improved steam pressure stability during peak demand
On older plants the hidden gain is plant life. Hotter return water is easier on metal than cold make-up water, so the system sees less stress on valves, pumps and seals.
Where recovery is lost on sites around Gauteng
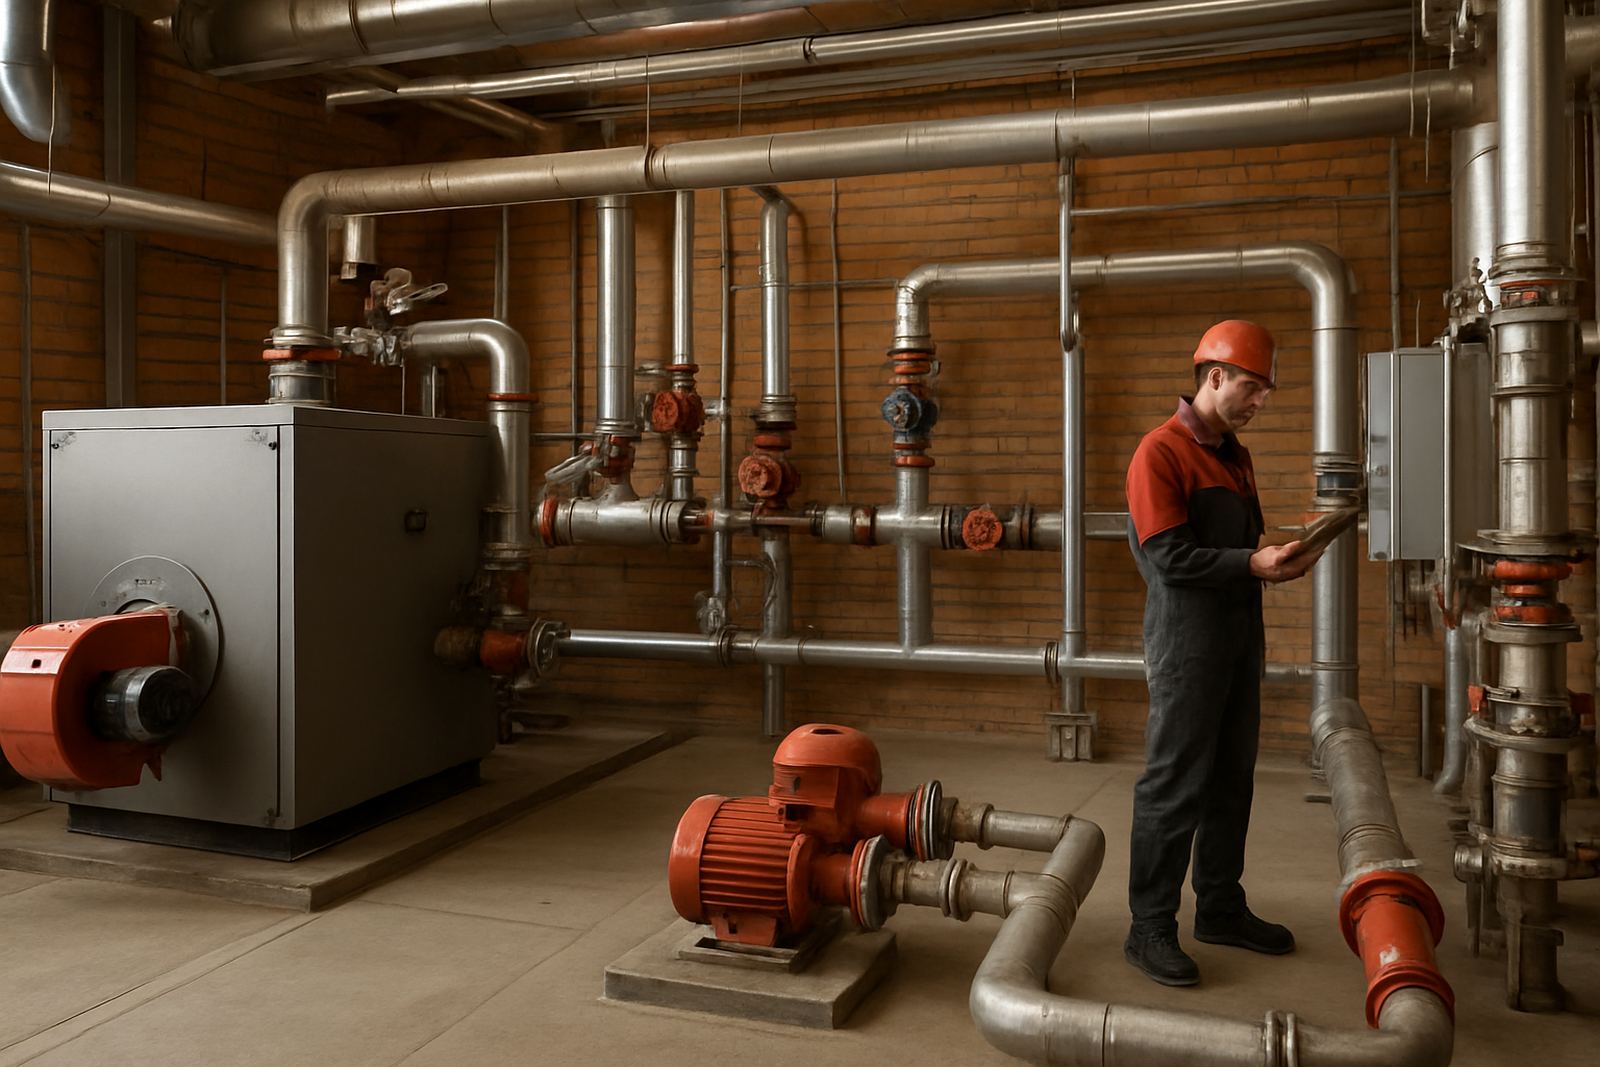
Most losses happen quietly. A steam trap fails open and discharges live steam. A return line is left uninsulated. A receiver tank overflows because the pump is undersized. Sometimes condensate is diverted because the return line has poor slope, air locks or contamination from process leaks. On industrial sites in Boksburg, Germiston and Kempton Park we often find that the biggest losses are not in the boiler house but out at the equipment.
If the plant handles food, laundry, chemicals or process heating, contamination must be checked before condensate is returned. A small oil leak or chemical carryover can damage a boiler quickly, so the recovery system must be simple to isolate and monitor. That is why maintenance and inspection are just as important as the pipework itself.
Practical checks before you chase savings
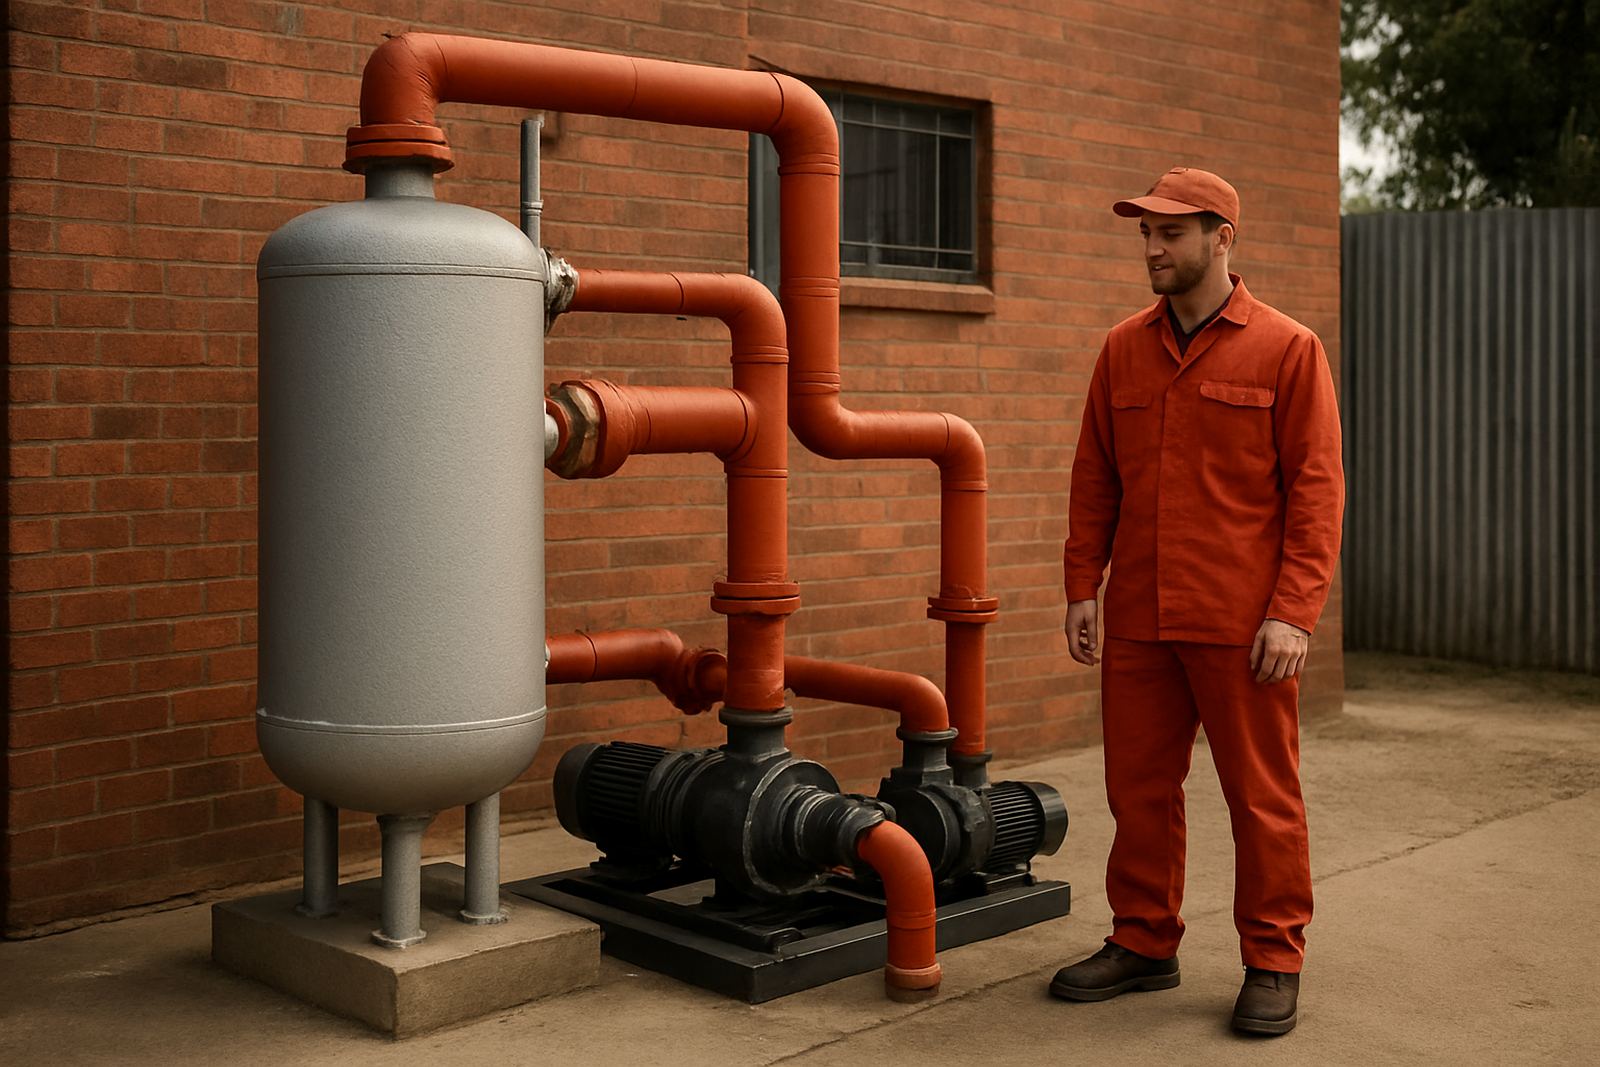
A proper condensate review starts with facts, not guesswork. Measure the return temperature, flow rate and where the losses are happening. Then look at the receiver capacity, pump condition, traps and the condition of insulation. If the plant uses a flash steam vessel, check whether that flash steam can be put to work on a deaerator, calorifier or low pressure user.
- Confirm the percentage of condensate currently returned
- Check trap condition on every major steam user
- Inspect return lines for leaks, corrosion and poor insulation
- Test receiver pumps, floats and level controls
- Verify water treatment settings for the higher return rate
In many cases, a modest repair programme gives a faster payback than a full rebuild. For sites with limited shutdown windows, phased work is often the best route.
A Pretoria example: less make-up water, steadier steam
A food plant in Pretoria North was sending most condensate to drain because the return line had repeated blockages and the receiver pump was undersized. The boiler house was also struggling during afternoon peaks, especially when the utility supply dipped and production restarted after interruptions. After the line was repaired, the receiver upgraded and the steam traps tested, the plant began returning most of its hot condensate to the boiler feed system.
The result was lower water purchase, less chemical dosing and a steadier boiler feed temperature. The site also saw fewer low-water alarms after start-up. Nothing dramatic changed on day one but over a few months the savings became visible on the utility bills and the boiler house ran with less strain.
How Ai-TEC approaches condensate return work
Condensate recovery only works when the boiler, pipework and treatment side all line up. Ai-TEC looks at the full steam circuit, from the process user back to the boiler feed system, then advises on the repairs or upgrades that make the most difference. That can include steam trap maintenance, calorifier checks, pump work, return line repair, combustion tuning and water treatment support.
Our teams in Gauteng and nationally handle sites from small commercial plants to heavier industrial operations. Based in Jet Park, Boksburg, we support emergency callouts, annual inspections and plant refurbishment where a site needs to recover heat instead of throwing it away. For a steam site, that is often the simplest way to cut running cost without changing the core process.
When a return system earns its keep
The best time to fix condensate recovery is before the boiler starts telling you about it through high fuel use, more blowdown or poor pressure control. A site that returns hot condensate, protects it from contamination and keeps the lines in good condition will usually spend less on water, chemicals and energy. It also gives the boiler a kinder feed supply, which matters when the plant has to keep going through load-shedding or after a weekend shutdown.
For many steam users, condensate is not a by-product. It is already paid for, already hot and ready to go back to work.